

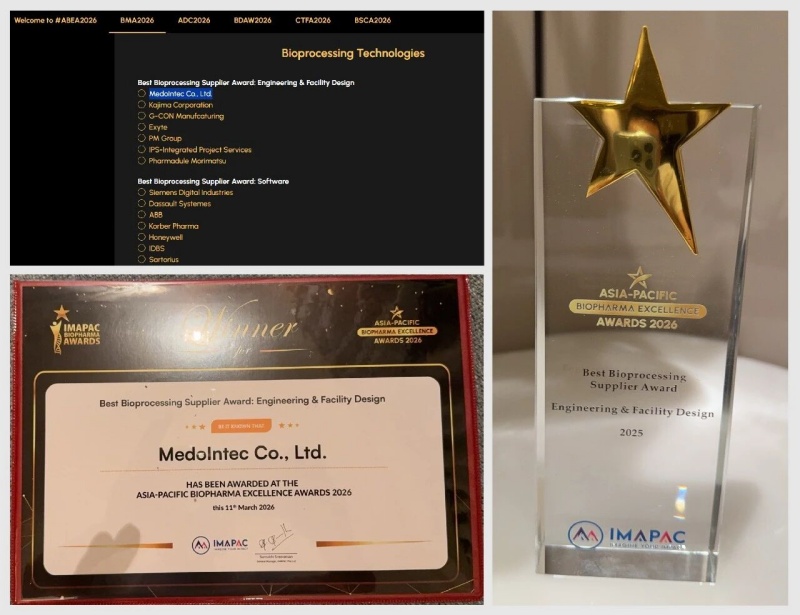
On 11th March 2026, at the award ceremony of the 2026 Asia-Pacific Biopharma Excellence Awards (ABEA2026) hosted by IMAPAC, a renowned consulting firm in the biopharmaceutical industry, in Singapore, Zhejiang MedoIntec Co., Ltd. was honored with the Best Bioprocessing Supplier Award: Engineering & Facility Design for its independently developed containerized modular cleanroom solution featuring flexible deployment and rapid scalability.
The 2026 Asia-Pacific Biopharma Excellence Awards (ABEA 2026) aims to recognize the annual outstanding achievements and leaders in the biopharmaceutical industry across the Asia-Pacific region, covering bioprocessing, supply chain, antibody-drug conjugates, clinical trials and other sectors, so as to stimulate innovation and lead the future of the industry.
MedoIntec’s innovative containerized modular cleanroom solution deeply integrates a high-standard clean environment with the unique mobility of containers, as well as the ease of renovation, upgrade and expansion enabled by modular construction, achieving a systematic breakthrough for clean facilities in terms of time, space and compliance. This international accolade is not only a high recognition of MedoIntec’s strength in the overall design, precision manufacturing and advanced clean technology of modular cleanrooms, but also an authoritative endorsement of its full-process professional capabilities from solution design to efficient project delivery.
Backed by 30 years of experience in GMP design and quality management in the pharmaceutical industry, MedoIntec has developed the containerized, flexible and movable modular “GMP Intelligent Clean Bio-module”, which provides a professional clean environment meeting the highest standard of Grade B+A cleanroom requirements in accordance with China’s 2010 GMP. While ensuring the stability of the clean environment, it also offers GMP pre-qualification services for equipment and the overall environment.
By integrating various process equipment (such as centrifuges, qPCR instruments, cell counters, bioreactors, etc.) and combining multiple grades of clean environments (Grade B+A, C+A, etc.), the solution can support a diverse range of applications, including somatic cell culture, virus/plasmid production, sterility testing of special preparations, and more.
In addition, the modular cleanroom is equipped with a full-stack intelligent management platform that integrates Building Management System (BMS), Environmental Management System (EMS), Access Control (AC), Closed-Circuit Television (CCTV), Electronic Lab Notebook (ELN) and Electronic Batch Record (EBR) functions, enabling convenient operation and maintenance. The electronic data and its integrity comply with the Appendix – Computerized Systems of China’s NMPA GMP 2010 Edition, meeting the full-process data integrity requirements from R&D to production, thus helping enterprises achieve asset-light operation and rapid commissioning.
The containerized modular cleanroom is mainly applied in three key scenarios:
- Providing a one-stop solution for in-hospital cell therapy centersfor hospitals, which greatly shortens the construction cycle, systematically solves process, compliance and operational challenges, and helps them quickly lay out the new track of cell therapy;
- Supporting high-end emerging start-ups in biopharmaceuticals, semiconductors and other sectors to rapidly establish compliant production capacity in a modular and low-investment manner, accelerating their commercialization process;
- Delivering shared GMP clean laboratoriesfor biopharmaceutical industrial parks, enabling start-ups to achieve a “plug-and-play”